

Use two measures for the line trial
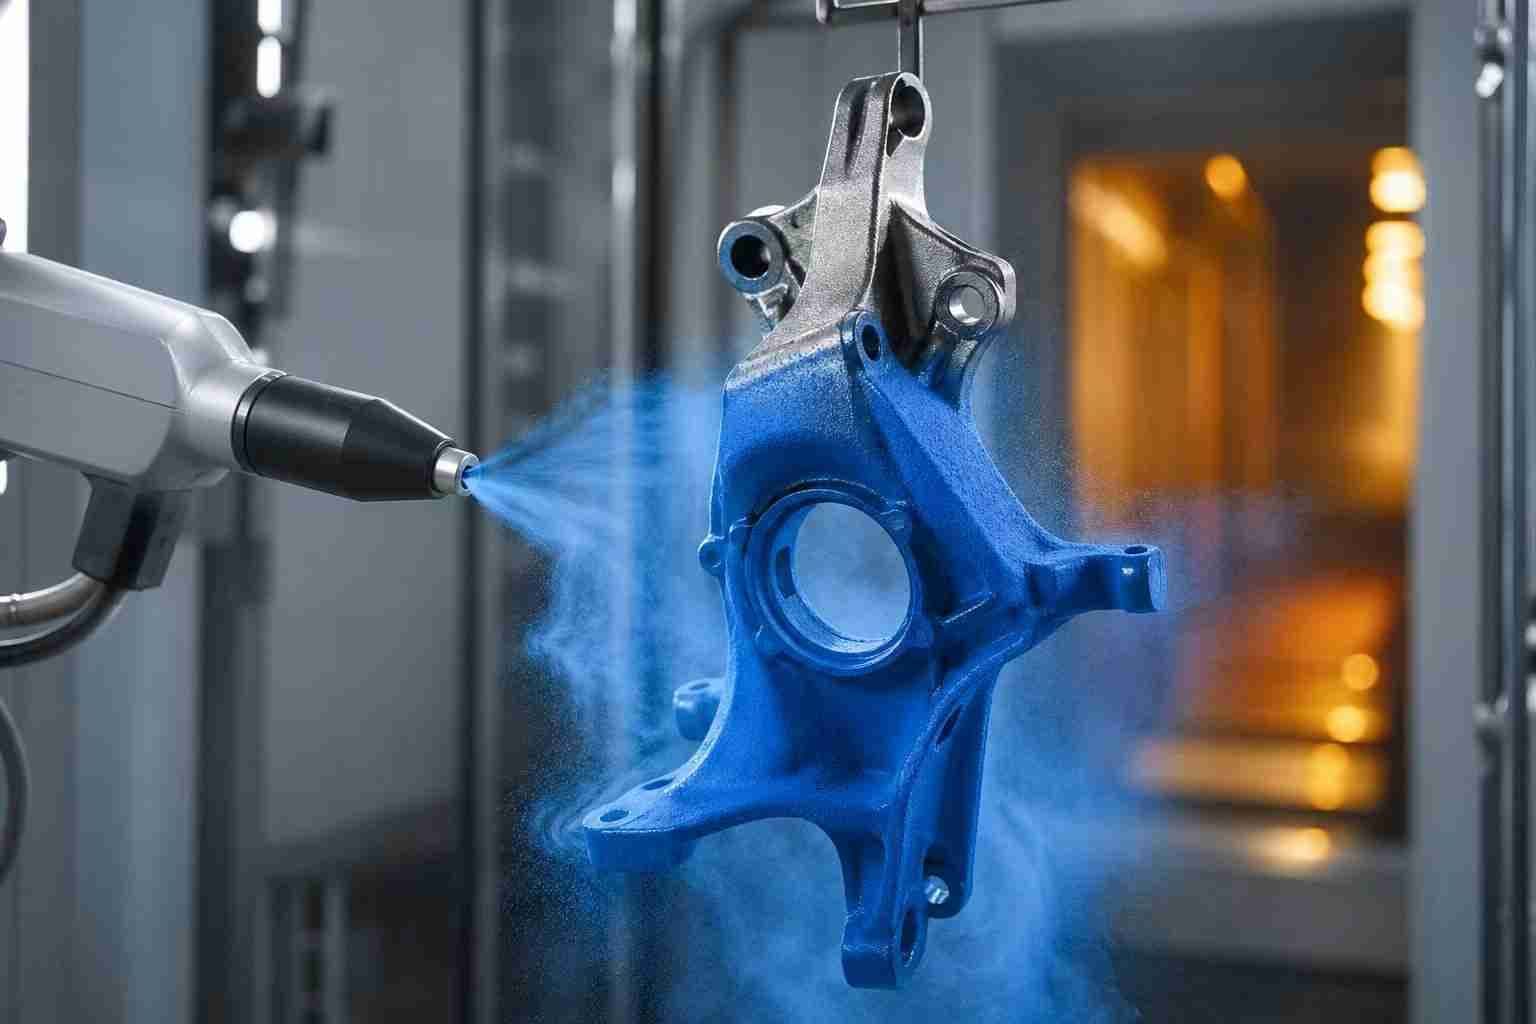
In its October 19, 2026 FABTECH announcement, PPG reported up to 85% first-pass transfer efficiency for its Envirocron HTE powder. First-pass transfer efficiency compares the powder that deposits on a part during the first application with the amount sprayed. It helps a coating team evaluate application performance.
When comparing powder options for a production order, also measure how much material the run consumes per accepted part. This second measure includes the powder used when parts need another coating pass and the material lost to disposal.
Weigh the powder at both ends of the trial
Choose a run boundary, such as one shift on one part family. Weigh the fresh powder issued to the run. Record the usable inventory inside the boundary before and after the run, including material in the feed and recovery system. Weigh any serviceable powder returned to stock and record the closing inventory after those returns. Where you cannot weigh residual material reliably, set up comparable start and end conditions.
Calculate net powder used as fresh powder issued plus opening usable inventory, minus closing usable inventory and serviceable returns. Treat reclaim recirculating within the booth as an internal movement and keep it separate from the fresh-issue total. Log powder sent to disposal as a loss within the run.
Divide by the parts that pass inspection
Use each released component once in the denominator, including parts accepted after rework. Record first-pass accepts, rework and final rejects separately so a change in yield is visible.
In an illustrative trial, the line receives 25 kg of fresh powder, starts with 4 kg of usable powder and ends with 5 kg after 3 kg of serviceable material is returned. Net use is 21 kg. With 100 accepted parts, this comes to 210 g per accepted part. Apply your actual powder price to that measured usage, and track labor and energy separately when comparing total finishing costs.
For a fair comparison, use the same part geometry, pretreatment, film-thickness targets and acceptance criteria. Check the finished parts for the specified film build, appearance, adhesion and cure. Record gun settings, recovery practice and any differences in the part mix that affect the result.
Plan a trial on representative steel parts
DAMEI's Container House Powder Coating is a polyester option for fabricated steel frames and panels. Include a representative frame and panel in the trial so the powder measurement reflects the work you will actually run. Contact DAMEI with the part dimensions, pretreatment, finish, target thickness, recovery setup and acceptance checks to discuss a candidate powder and sample plan.